Anatomy of the Reducer and Its Four Challenges
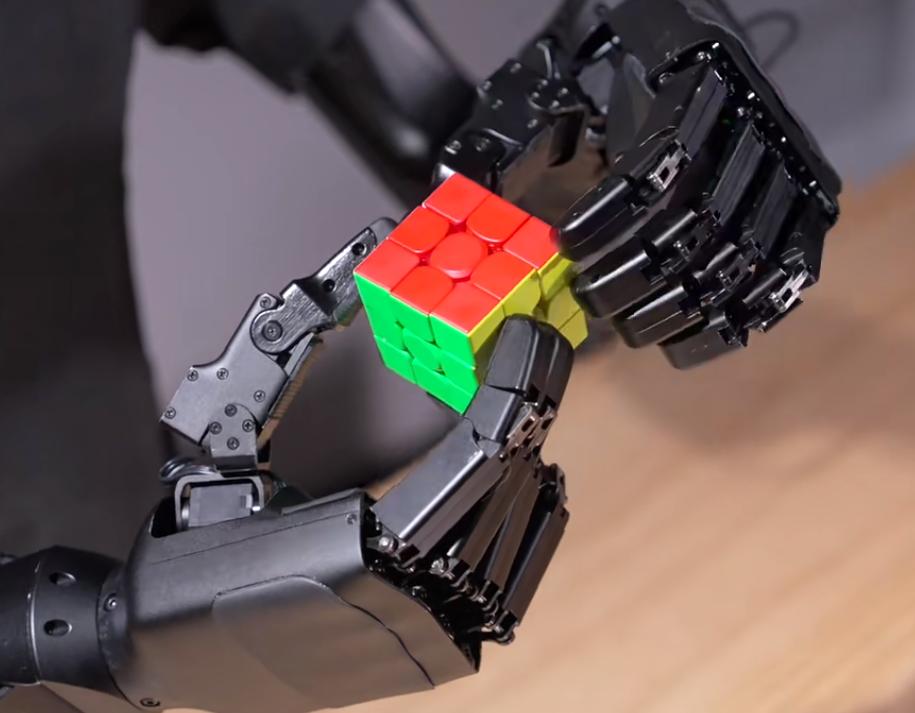
A planetary reducer for a dexterous hand is built from a sun gear, three to four planet gears, a fixed internal ring gear, and a carrier. The source lists four lubrication challenges that make this component unlike an industrial gearbox: the grease volume is minimal, the joint reverses at high frequency under alternating peak load, heat dissipation is poor inside a sealed finger module, and overload impacts arrive with every grasp and release. Each challenge alone is manageable; together they define a narrow operating window.
Contact Pressure and Subsurface Stress
The source notes contact pressures in the 1-3 GPa range at the tooth meshing interface, and explains that the maximum shear stress develops 0.5-1 mm below the surface. This subsurface location is why pitting begins invisibly: the material is stressed below the visible surface, and only later does the surface break open. The pitting sequence runs from initial surface fatigue to micro-pitting, then spalling, and eventually tooth fracture if left unchecked. By the time noise is audible, the damage has been growing for thousands of cycles.
How the Chain Starts: Throw-Off, Heat and Contamination
In a rotating planetary stage, centrifugal force throws grease away from the meshing zone, so a grease with adhesion and centrifugal resistance is required, a requirement unique to planetary configurations. If the grease film fails, the source reports bearing temperature can climb from 50°C to above 90°C within 15-30 minutes. Dust ingress is flagged as able to cut component life by more than 80%, which is why sealed joints must not lose their grease seal. The economic consequence is severe: repair or replacement cost is cited at 50-200% of the original unit cost, which is why early failure is so expensive in a product with many joints.
High-Temperature and Shear Demands
Long continuous runs can push a dexterous-hand joint toward 150°C, while typical mineral-oil greases have dropping points at or below 200°C, leaving little margin. The source therefore highlights EP additives that form FeS and FePO4 reaction films, and warns that shear-thinning of the thickener under high-frequency reversal degrades film replenishment over time. A grease chosen for one property alone, for example very low viscosity for speed, fails the other three challenges.
Validation / Selection Conclusion
Validate the grease with a forward-reverse cycling test that reproduces the alternating peak load, monitor bearing temperature rise, and inspect for throw-off inside the sealed cavity. The acceptance criteria should include EP performance under 1-3 GPa contact, stable structure under shear, adhesion that resists centrifugal throw-off, and a dropping point comfortably above the joint’s sustained temperature. The failure chain to interrupt is pitting first, because once pitting starts, noise and precision loss follow predictably.