By VNOVO Technical Support Team
Food and beverage processing equipment operates where lubrication failure is not merely a maintenance issue — it is a food safety event Food-grade grease, registered to NSF H1 for incidental food contact with ingredients that comply with FDA 21 CFR 178.3570, is the baseline for any lubrication point where accidental contact with product or packaging is geometrically possible.
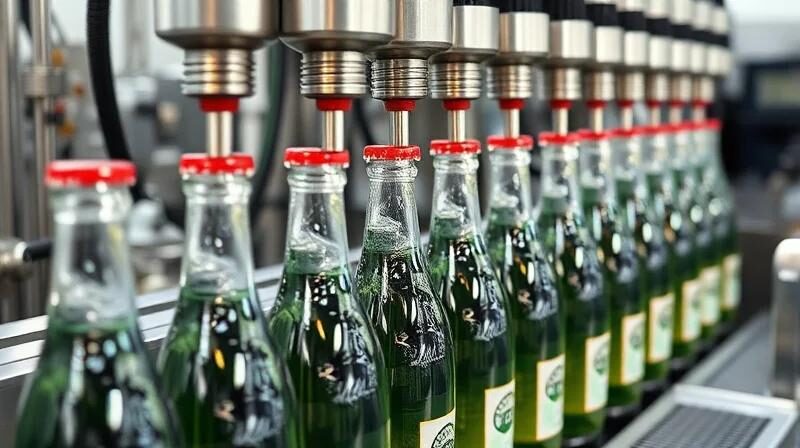
What Makes Food and Beverage Equipment Lubrication Demanding?
– Incidental food contact is unavoidable. Even sealed bearings can leak. Any lubricant where exposure is foreseeable must be food-grade.
– Frequent washdown with caustic chemicals at up to 85-90 degC strips conventional greases from surfaces.
– Wide temperature transitions within a single process line — from frozen storage at -20 degC through cooking or pasteurization at 80-120 degC.
– Regulatory compliance is tied directly to the lubricant. NSF H1 registration and ISO 21469 certification document that lubricant ingredients have been reviewed for incidental food contact safety. Non-listed ingredients — — create regulatory exposure.
– Food debris and moisture accumulate on migrated grease, creating hygiene risks beyond the lubrication function itself.
– Kosher and Halal requirements may apply simultaneously, requiring the more restrictive certification in addition to NSF H1.
Why Do Food-Grade Grease Problems Persist Even When Food-Grade Lubricant Is Specified?
1. H2 grease used in an H1 exposure zone. H2-rated greases (no food contact permitted) provide no regulatory protection if a seal fails in a product zone.
2. Wash-off during CIP/SIP cycles. Even NSF H1 greases vary in water resistance. Low-quality greases lose thickness during washdown and migrate from bearing cavities.
3. Thermal degradation. Some greases soften above 80 degC, losing film strength; others harden permanently after high-temperature exposure.
4. Incompatibility with seals and surface finishes. Some greases contain additives that attack stainless steel passivation or degrade NBR, FKM, or silicone seals.
5. Bleeding and migration into product zones. High oil bleed at operating temperature migrates along shafts or weeps through seals into product areas.
6. Cross-contamination from storage and handling. Shared grease guns and non-dedicated lubrication stations create accidental contamination between food-grade and industrial greases.
7. Religious certification gaps. Kosher or Halal certification may have lapsed.
What Properties Make Food-Grade Grease Suitable for Food and Beverage Equipment?
– NSF H1 registration with FDA 21 CFR 178.3570 compliance. All ingredients — base oil, thickener, and additives — must be on the approved list. Any unlisted additive creates regulatory exposure.
– Water and washdown resistance. Synthetic base oils — PAO, synthetic esters, or silicone — provide superior water resistance to white mineral oil. High dropping point maintains consistency through CIP cycles.
– Thickener system matched to temperature range. Aluminum complex: wide range, water resistant, general processing. Polyurea: superior high-temperature stability, cooking and pasteurization. PTFE-based: food equipment compatibility, smooth texture.
– Seal and surface compatibility. NBR, FKM, silicone, and EPDM seals; stainless steel; polymer coatings.
– Wide service temperature range for process lines spanning cold storage to thermal processing.
– ISO 21469 certification for manufacturing hygiene — requiring annual facility inspection beyond NSF H1 registration.
– Kosher and Halal certification where required.
How to Select the Right Food-Grade Grease for Food and Beverage Equipment
Step 1 – Identify equipment conditions:
| Equipment Zone | Temperature Range | Key Requirement |
| Cold storage / chilling | -20 degC to 4 degC | Low-temp pumpability, NSF H1 |
| Ambient processing / filling | 4 degC to 40 degC | Water resistance, wide temp range |
| Cooking / pasteurization | 80 degC to 120 degC | High dropping point, thermal stability |
| Sealed gearboxes (exposed) | 40 degC to 80 degC | H1 where exposure possible, EP additives |
| Conveyor guides / sliding | -10 degC to 60 degC | Adhesion, anti-fling, water resistance |
Step 3 – Verify: Confirm NSF H1 registration number in the NSF White Book. Confirm FDA 21 CFR 178.3570 compliance for all ingredients. Confirm ISO 21469 certification scope. Confirm Kosher or Halal certification where required. Confirm material compatibility with seals and finishes.
Quick Reference: Food-Grade Grease Selection for Food and Beverage Equipment
| Application | Priority | Recommended Direction |
| Cold storage / chilling | Low-temp pumpability + water resistance | Synthetic ester-based H1 grease, low-temp grade |
| Ambient processing / filling | Water resistance + wide temp range | Aluminum complex thickener, PAO or white oil base, NSF H1 |
| Cooking / pasteurization | High-temp stability + drop point | Polyurea thickener, synthetic ester base, >260 degC drop point, NSF H1 |
| Sealed gearboxes (exposed) | EP performance + food safety | PAO-based H1 grease with EP additives, ISO 21469 certified |
| Conveyor guides / sliding | Adhesion + anti-migration | Tacky PAO-based H1 grease, anti-fling additive |
| Seals / O-rings (food zone) | Material compatibility + food safety | PTFE or silicone-based H1 grease, seal-compatible |
How VNOVO Provides Technical Support
VNOVO does not supply a single universal food-grade grease:
Application-Oriented Selection Guidance: VNOVO reviews your equipment temperature profile, washdown frequency, food exposure zone classification, and seal materials, recommending thickener type, base oil chemistry, viscosity grade, and required food safety certifications.
Regulatory Compliance Verification: VNOVO confirms current NSF H1 registration, FDA 21 CFR 178.3570 ingredient compliance, ISO 21469 scope, and current Kosher or Halal certification.
Scenario-Based Communication Support: VNOVO explains trade-offs (white mineral oil base = cost-effective but lower thermal stability vs. PAO base = superior stability and water resistance; aluminum complex thickener = wide range vs. polyurea = superior high-temperature performance) and what verification steps to prioritize.
Conclusion
When to use food-grade grease in food and beverage equipment
When any lubrication point is geometrically exposed to product or packaging — including sealed bearings above open product zones, conveyors through processing areas, or any equipment where seal failure could introduce lubricant into the product stream. When washdown frequency or temperature profile exceeds conventional grease capability, or when regulatory compliance requires documented food safety justification.
When an alternative lubricant may be more appropriate
When the lubrication point is confirmed H2 — full mechanical enclosure verified and documented segregation from any food zone. When the equipment operates in a non-regulated area with no certification requirements — conventional industrial grease may be sufficient and more cost-effective.
What VNOVO can support
1. Selection guidance — translating equipment conditions, food exposure classification, and certification requirements into thickener type, base oil, and viscosity grade
2. Regulatory alignment — confirming NSF H1 registration, FDA 21 CFR 178.3570 ingredient compliance, ISO 21469 certification scope, and Kosher or Halal certification where required
3. Scenario communication — providing the technical rationale for formulation recommendations and clarifying trade-offs between base oil chemistries and thickener systems in your compliance documentation
This article is provided for informational purposes based on industry references and food-grade lubricant knowledge. Specific food-grade grease selection should always be verified through equipment manufacturer confirmation, NSF registration validation in the NSF White Book (info.nsf.org), and material compatibility testing for your specific equipment seal and finish materials.